Microinverter Batch Acceptance Sampling: A Distributor’s ISO 2859-1 Inspection Plan
Turn an approved OEM sample into a repeatable shipment-release gate: define lots, select units randomly, classify defects and retain serial-level evidence.

TMG Technical Team
Quality & Applications Engineering

A distributor approves an OEM microinverter sample, then receives 800 production units six months later. The cartons look right, but is the shipped firmware still the approved version? Are the connectors, labels and gateway instructions consistent across the lot? A golden sample cannot answer those questions by itself. The missing control is a written batch acceptance plan agreed before production.
This guide is for purchasing and quality teams, not a substitute for a licensed sampling standard, accredited safety testing or an agreed contract. It describes how to specify the inspection; it does not supply ISO acceptance tables or claim that a small sample proves every unit safe.
Freeze the approved configuration first
The OEM sample evaluation plan ends with a golden sample, controlled bill of materials (BOM), firmware baseline, manuals and packaging. Convert that approval into a revision-controlled comparison sheet for the production lot:
| Controlled item | Reference to freeze | Production evidence |
|---|---|---|
| Product identity | Exact model suffix and electrical rating | Label and packing list |
| Hardware | BOM revision, connectors, cable and enclosure | Manufacturing change record |
| Software | Firmware build, grid profile, gateway compatibility | Device readout and release log |
| Documentation | Market language, wiring diagram, warnings | Printed pack and digital revision |
| Traceability | Serial format, date/line/batch relationship | Complete serial-number export |
| Pack-out | Accessories, carton and pallet specification | Packing record and sampled cartons |
Do not silently treat a substitute connector, grid profile or firmware as a cosmetic deviation. Put the change through the firmware and product change-control process and recheck affected market evidence before shipment.
Define what counts as one lot
The ISO 2859-1:2026 overview describes lot-by-lot inspection by attributes using AQL-indexed sampling schemes. Before anyone selects a sample, the buyer and factory must agree the lot boundary. A purchase order is not automatically a homogeneous lot.
For example, an 800-unit order may need separate lots if it spans a hardware revision, production line, firmware build, connector supplier or country-specific label. Record quantity, serial range, production dates, line, approved configuration and any rework. Keep rejected and reworked units distinguishable. Otherwise a random sample from one pallet may miss a changed subpopulation elsewhere in the shipment.
Select samples from the whole defined lot, using a documented random method across cartons and pallets. Do not let the factory present only hand-picked “inspection units.” Record sampled serials, carton locations, selection method, inspector and time. If units have already been segregated by revision, inspect those as distinct lots rather than blending the results.
Choose the sampling plan before seeing defects
State the exact ISO 2859-1 edition, inspection level, normal/tightened/reduced status, defect-class AQLs, single/double/multiple plan if applicable, sample size, and acceptance/rejection numbers from the licensed standard. The 2026 edition replaced the earlier edition and includes updated switching and skip-lot provisions; do not copy an old AQL chart into a new contract without checking the edition.
An AQL is an index for a sampling scheme, not a promise that every accepted shipment contains that percentage of defective units. Acceptance sampling also does not replace supplier process controls or 100% production tests. Set the plan before inspection so a supplier cannot change the sample size after seeing an unfavorable result.
Use risk-based defect classes. The following is a buyer-policy example, not ISO's mandatory classification:
| Class | Microinverter example | Proposed disposition |
|---|---|---|
| Critical | Exposed live-part risk, wrong safety-critical component, missing protective marking | Stop release, quarantine lot, investigate affected population |
| Major | Wrong model/rating, incompatible connector, wrong grid-profile build, failed approved functional check | Reject or hold pending documented containment and resampling agreement |
| Minor | Cosmetic finish or noncritical pack-out discrepancy within agreed limits | Apply the pre-agreed acceptance plan and corrective action |
One observed critical issue should trigger containment; calling it “zero-tolerance” is a contractual escalation rule, not proof that unsampled devices are defect-free. Safety conformity belongs to the applicable test/certification route. IEC 62109-1 sets general PV power-converter safety requirements, while IEC 62109-2 addresses inverter-specific requirements. Verify the edition and scope required in the destination market and the exact tested model; a warehouse inspector must not improvise dielectric, grid-fault or destructive tests.
Split documentary, visual and functional checks
Some checks should cover every unit by factory record: unique serial assignment, completed end-of-line test record, configuration association and pass/fail status. The distributor should reconcile the entire serial list to cartons and shipment quantity, then audit selected source records. A sampled visual inspection cannot repair a missing population-wide traceability file.
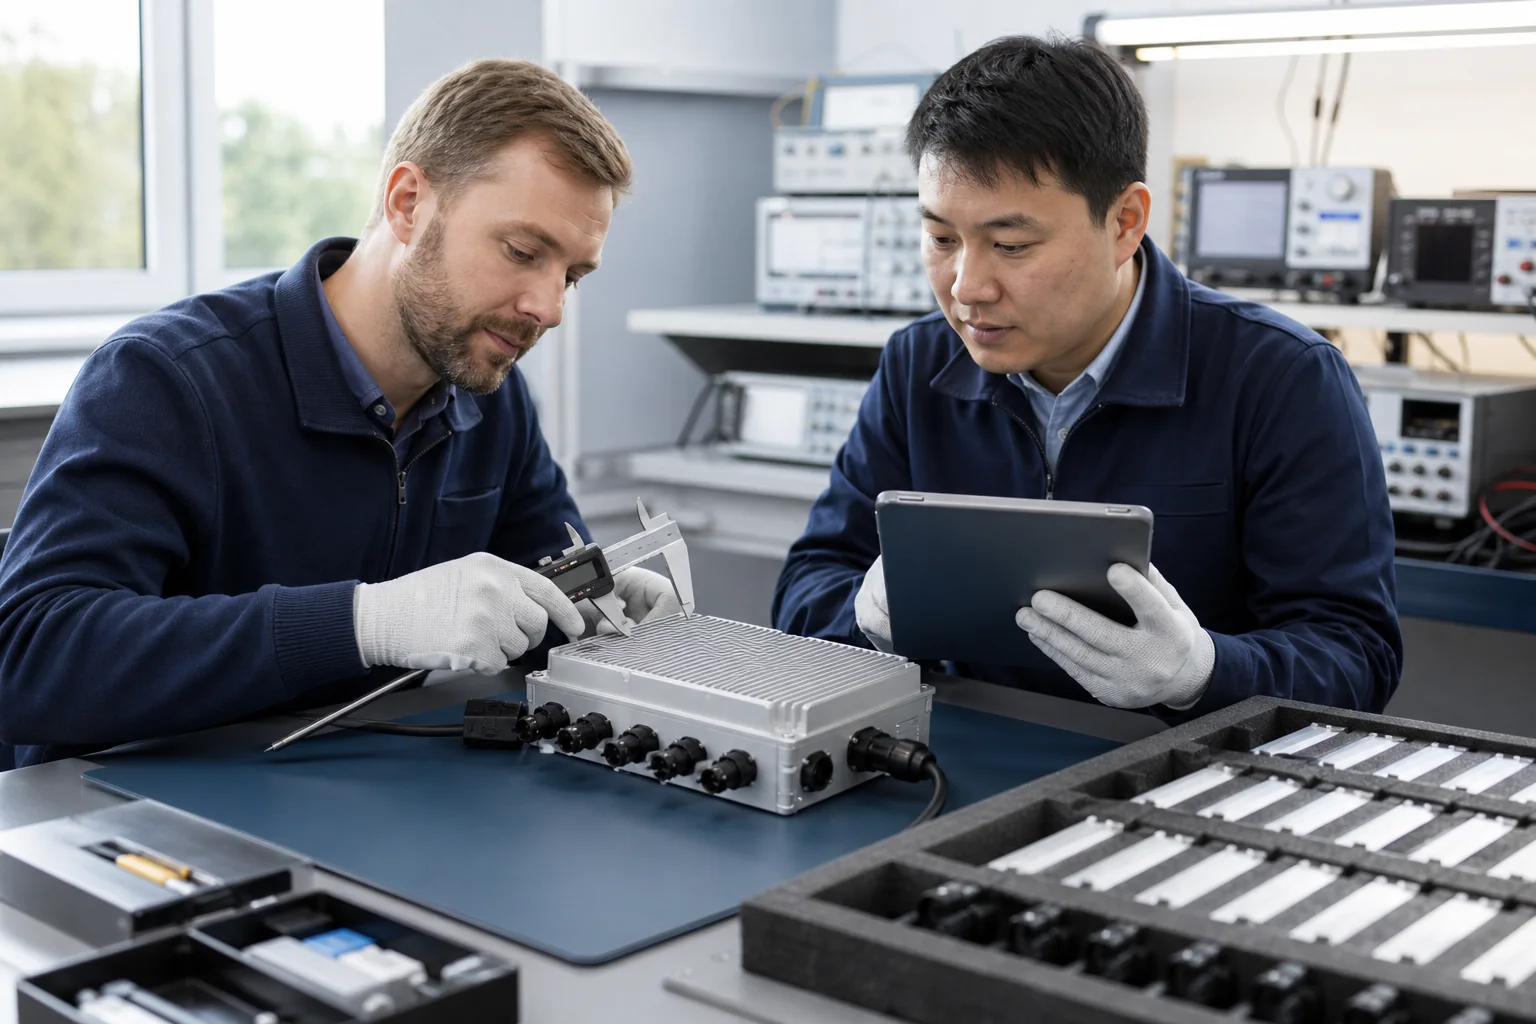
On sampled units, inspect identity, connector type/keying, cable strain relief, enclosure/fasteners, sealing appearance, label legibility, accessories, carton protection and matching manuals. Use a signed photo reference, not “looks acceptable.” For functional observations, use a qualified test setup, approved procedures and conditions within the exact model's stated limits. Record instrument IDs, firmware readout, input/grid conditions, observation duration, result and raw file. Separate buyer observations from accredited compliance tests.
The IEA PVPS technical-assumptions report identifies a procurement gap where factory inspection or product testing is not specified, leaving room for batch-specific manufacturing deviations. That is a reason to define this gate in the RFQ, not evidence of a defect rate for this product.
Write the fail-and-release decision tree
For each failed unit, record serial, defect class, photo or log, exact acceptance criterion and affected configuration. The response should follow a pre-agreed path:
- Hold the lot and stop shipping if a critical or systemic discrepancy appears.
- Contain by serial, BOM, firmware, line and time window; inspect the suspected subpopulation.
- Correct the root cause and document rework or replacement under controlled instructions.
- Reinspect under the agreed standard and contract; do not mix repaired units into an untouched lot without clear identification.
- Release only after buyer sign-off on the report, deviations and shipment serial list.
Decide in the purchase agreement who pays for independent inspection, rework, repeat testing, freight delay and rejected stock. “Conditional release” should name the approved deviation, affected serials, market, expiry and owner; a verbal concession is not a release record.
After delivery, use the RMA root-cause evidence checklist to compare field cases with production batches. If transit damage is suspected, consult the export packaging qualification guide rather than classifying it automatically as a factory defect.
Add a one-page batch gate to the RFQ
Ask for the controlled sample and BOM, proposed lot definition, complete serial/EOL data, licensed sampling-plan reference, defect taxonomy, test capability, third-party inspection access, hold/rework rules and release authority. For private-label orders, ensure the serial system survives branding and that labels match the approved market configuration. The OEM distributor solution gives context for that handoff.
Send TMG the destination market, exact model/configuration, order size, branding scope and proposed inspection method through TMG Contact. A useful quotation should make the batch gate and unresolved evidence explicit; it should not imply that an AQL label alone guarantees safety or reliability.
Sources & further reading
- https://www.iso.org/cms/live/live/en/sites/isoorg/contents/data/standard/08/54/85464.html
- https://webstore.iec.ch/en/publication/6470
- https://webstore.iec.ch/en/publication/6471
- https://iea-pvps.org/wp-content/uploads/2020/01/Report_IEA-PVPS_T13-08_2017_Technical_Assumptions_Used_in_PV_Financial_Models.pdf
Last reviewed October 1, 2026.